
Approved procedures only
Welding procedures (WPS) move from draft to approved to withdrawn. A change creates a new revision; an approved procedure is never edited in place.
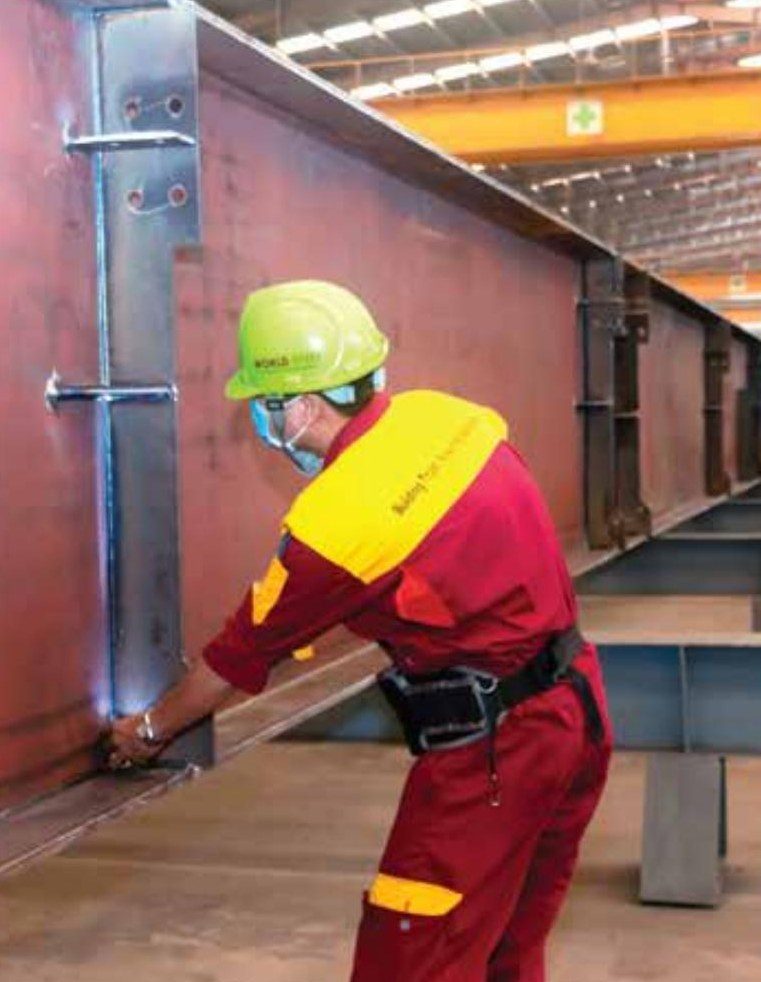
BOM Studio · Quality
Quality is not a certificate at the end of the project. In BOM Studio, inspections are built into the production route of every member. A member that is finished is not passed until a QC inspector records the result, a failed inspection stays on the record, and nothing leaves the factory with an open non-conformance.
Screens
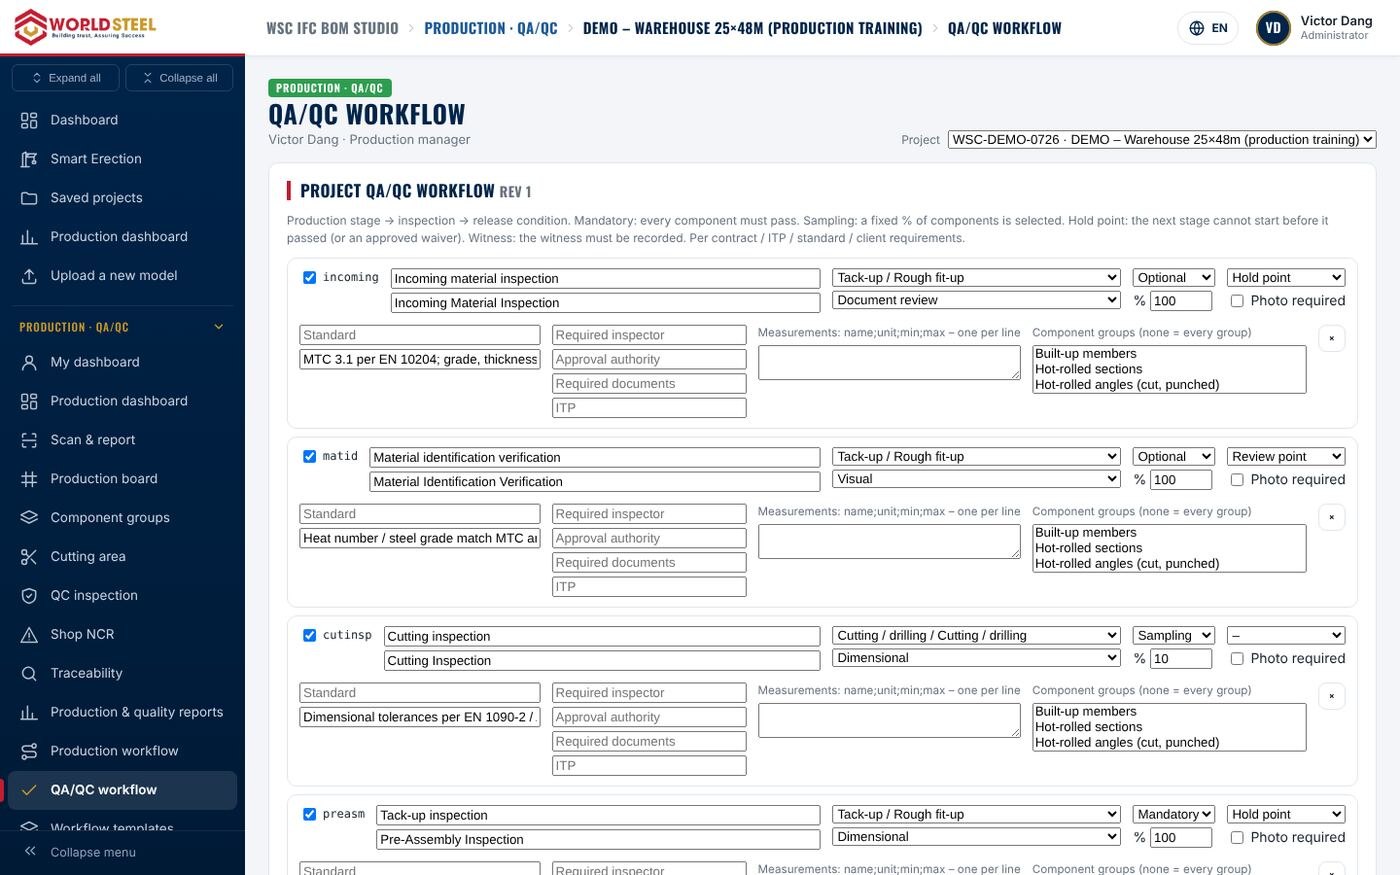
For each project, QA/QC sets the inspection steps between production stages: incoming material, fit-up, visual weld inspection, UT / MT, surface preparation, coating thickness and release for shipping.
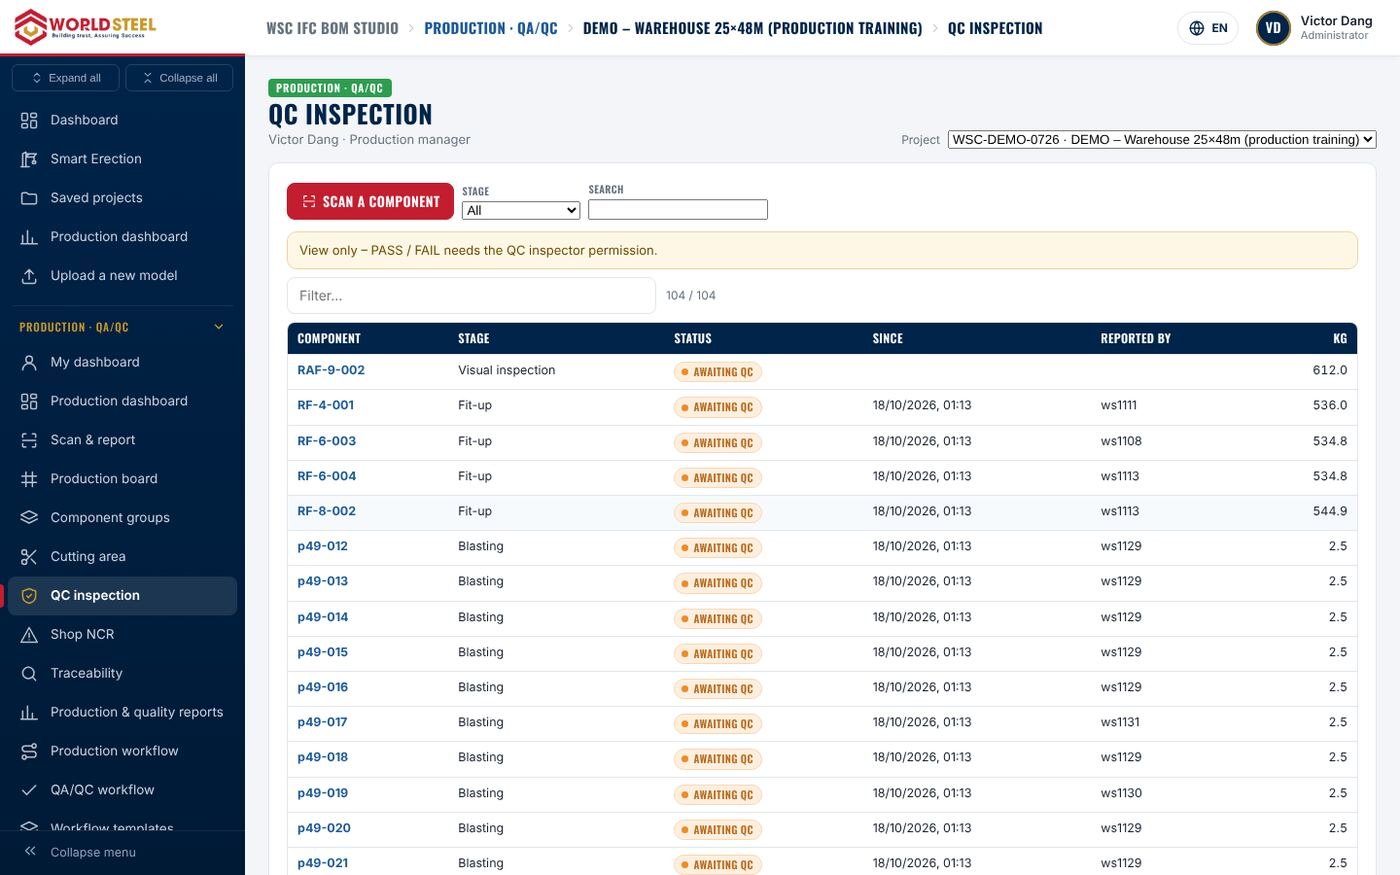
Finished members appear in the QC inspection queue with their stage, the time they were reported and who reported them. Only a user with the QC inspector permission can record PASS or FAIL.
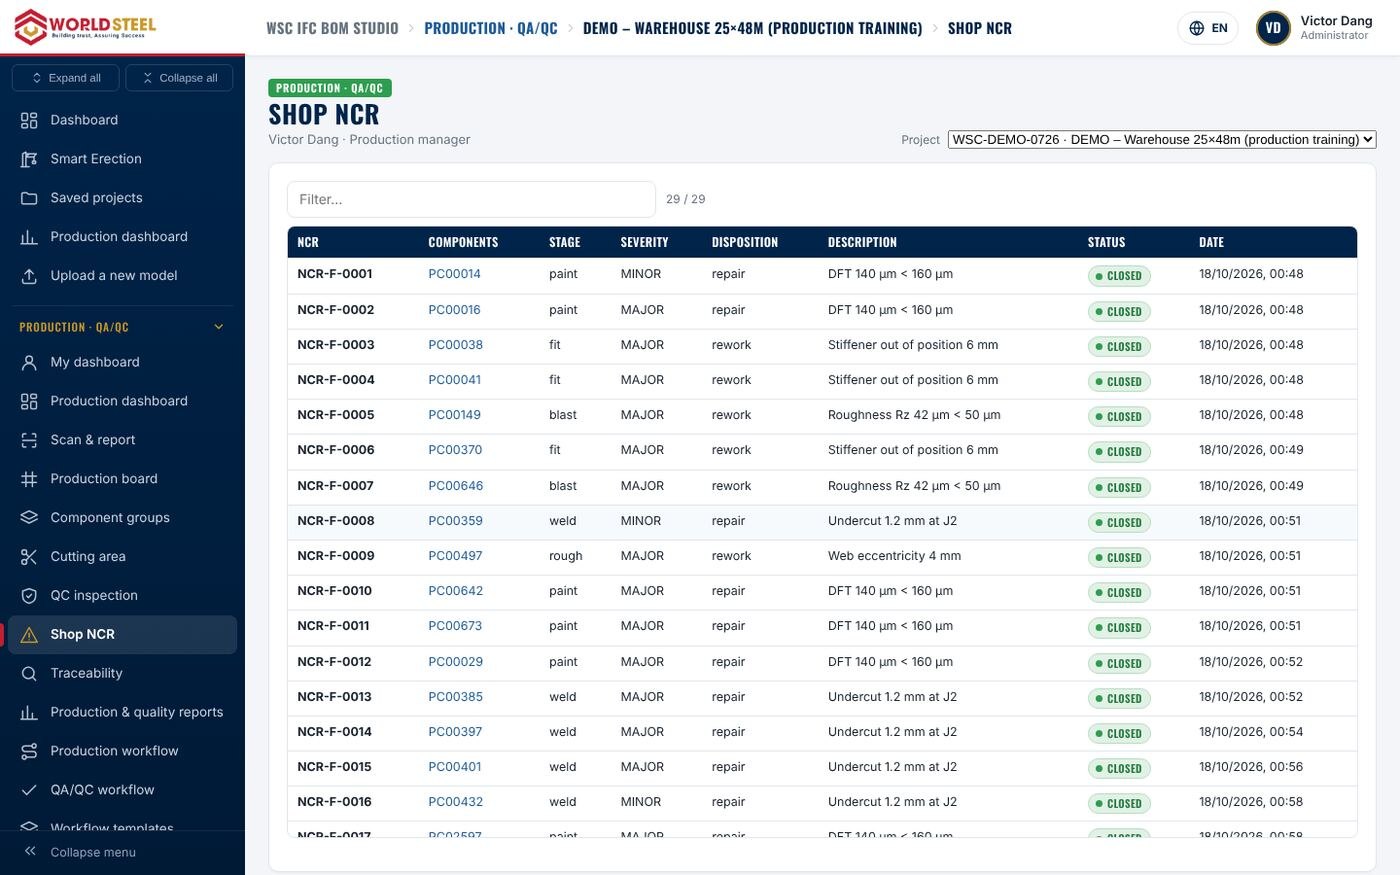
Every non-conformance is logged with the member, stage, severity, disposition and description, and stays on record after it is closed.
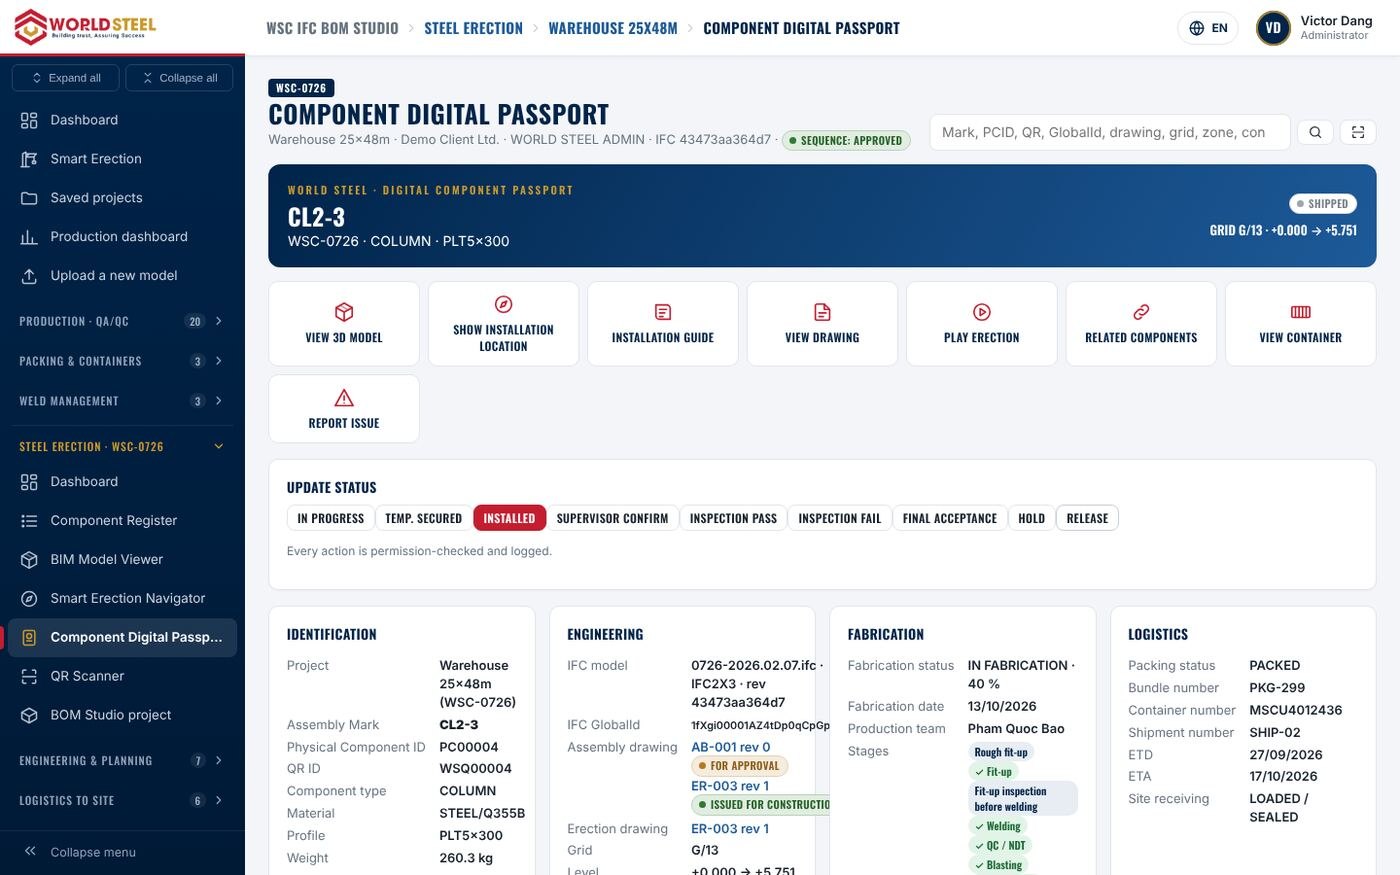
The member's record shows its inspections with the rest of its history: production, welding, packing and position in the building.
The Rules
When a step with an inspection is finished, the member moves to "Awaiting QC". Only a QC inspector can record PASS or FAIL, and the next stage cannot start beyond the quantity QC has accepted. A failed inspection is recorded with the defect and the action taken, and the re-inspection after repair is recorded as a new inspection (#2, #3), so the history is complete.
The people who report production cannot approve QC, and the people who update erection cannot accept their own work. This separation is built into the permissions, not left to good intentions.
Rules built into the system
Performed directly by World Steel
Every step is recorded with who, when and what.
The team scans the member and confirms the finished step.
Related documents: Production record
The member waits in the QC inspector's queue.
Related documents: Inspection queue
The inspector checks to the standard in the route, with measurements and photographs where required.
Related documents: Inspection record
PASS releases the member to the next stage. FAIL records the defect and the action: rework, repair, accept with approval or reject.
Related documents: Result with defect type
A non-conformance moves from Open to In progress, Awaiting re-inspection and Closed, and only QC can close it. The repaired member is inspected again and the new result is added to its history.
Related documents: NCR record, inspection #2, #3
Only members released by QC, painted and free of open NCRs can be packed for shipping.
Related documents: Release for packing
Welding
Welding is where traceability matters most. BOM Studio checks it at every scan.
Welding procedures (WPS) move from draft to approved to withdrawn. A change creates a new revision; an approved procedure is never edited in place.
A welder can only report welding under a procedure they are authorised for. The server rejects a welder whose certificate has expired, whose continuity lapsed for more than six months, or who is outside the qualified range.
Each weld report records the welder, the procedure and its revision, the data needed for the weld traceability section of your Manufacturer's Data Report.
The welding engineer sees certificates that are expired or about to expire before they affect production.
Records are append-only, with the value before and after every change.
| Question | Where the answer comes from |
|---|---|
| Who made this member, and when? | The member's timeline: every production step, team and date |
| Which procedure was this weld made to? | Weld report: welder, WPS and revision |
| Which inspection did it pass, and at which attempt? | Quality history of the member (PDF): FAIL #1, PASS #2 |
| Which members did this welder work on? | Search by welder, team, WPS or date range |
| Are any members still on hold? | QC queue and open NCRs, by project |
FAQ
Straight answers on scope, design codes, shipping and what happens in Guyana.
Ask an engineerYes. Witness points can be set in the QA/QC route for your project, and you can follow the results in BOM Studio. You can also book a live online audit of our factory.
Each inspection step names its standard, for example ISO 5817, AWS D1.1, AS/NZS 1554.1 or EN 1090-2, according to the requirements of your project.
The failure is recorded with the defect and the action taken. The member cannot move on until it is repaired and passes a new inspection, and both results stay in its history.
No. Packing only accepts members that are finished, released by QC, painted and free of open NCRs. The system checks this, not a person with a list.
Yes. Inspection records, NCRs and weld traceability are part of the project record and of the handover package.
Tell us about your project and its standards. We will show you how inspections and hold points would be set up and reported.
World Steel's own project platform. Every steel member has an ID and QR code, and every step from production to handover is recorded, so you can follow your pr…
Read moreFollow the fabrication of your building live: progress by steel weight for every stage, a coloured 3D model, factory photographs and weekly reports from a secu…
Read moreQR scan packing of QC-released members, checked container load plans, locked packing lists, a QR code on every package and a full report for every container.
Read moreTraceability that continues on site: component passports by QR code, model navigation, erection sequence, 4D progress, site inspections and an offline site app…
Read moreA complete, verifiable record of your building, generated from the project data and locked with a SHA-256 manifest.
Read moreThe risks of an overseas steel project, from model errors to missing members on site, and how BOM Studio controls each one with a check, a rule and a record.
Read moreTraceability, welding control, inspection and test plans, NDT, coating inspection and the quality records you receive with every shipment.
Read moreEvery member inspected, marked, listed, packed, loaded and photographed: how World Steel makes sure your project in Guyana receives exactly what was designed, …
Read moreThe international shipping lines, routes and transshipment hubs that connect Vietnam with Georgetown, the weekly sailing rhythm, a realistic 45–60 day transit …
Read more